| Load Capacity |
Rated static load should exceed the intended firearm and accessory load by at least 25%; deformation should remain within the buyer’s specified limit. |
Review load-test reports, fixture drawings, safety factor calculations, and independent samples tested at the maximum rated load. |
15% |
0–10 |
| Recoil and Fatigue Resistance |
The product should pass a documented cyclic-load or recoil-simulation program based on the intended weapon platform; no cracking, loosening, or loss of adjustment is acceptable. |
Require a buyer-approved test protocol, pre-test and post-test dimensional checks, fastener-torque records, and failure analysis where applicable. |
15% |
0–10 |
| Rail and Interface Compatibility |
For Picatinny interfaces, dimensional claims should reference MIL-STD-1913 or STANAG 4694 as applicable; mounting geometry must match the specified rail profile. |
Check controlled drawings, gauge inspection records, interchangeability tests, and fit verification on representative rails. |
10% |
0–10 |
| Environmental Durability |
Testing should cover applicable temperature, humidity, vibration, shock, dust, and rain conditions using the relevant methods of MIL-STD-810H or an equivalent customer-defined program. |
Verify the test method, severity level, sample configuration, calibration records, and before-and-after functional results. MIL-STD-810H is a test-method framework, not a blanket product certification. |
15% |
0–10 |
| Corrosion Protection |
Material and coating systems should be selected for the operating environment; salt-spray duration and acceptance criteria must be agreed before testing. |
Review coating specifications, surface-treatment records, coating-thickness measurements, and testing under ISO 9227 or ASTM B117 where relevant. Salt spray alone does not predict every field environment. |
10% |
0–10 |
| Materials and Manufacturing Control |
Material certificates, heat or batch traceability, controlled machining parameters, and inspection plans should be available for load-bearing components. |
Audit incoming-material records, CNC inspection reports, hardness or alloy verification, welding qualifications where applicable, and nonconformance records. |
10% |
0–10 |
| Quality Management System |
A current ISO 9001 certificate from an accredited certification body is a useful baseline for document control, corrective action, inspection, and process management. |
Confirm certificate scope, validity, issuing body accreditation, production-site address, internal audit records, and corrective-action effectiveness. |
10% |
0–10 |
| Dimensional Inspection and Calibration |
Critical dimensions should have defined tolerances, measurement methods, and calibrated equipment. ISO/IEC 17025-accredited laboratories are preferred for independent testing. |
Check calibration certificates, gauge traceability, first-article inspection reports, capability studies, and independent laboratory accreditation scope. |
5% |
0–10 |
| Ergonomics and Field Operation |
Adjustment controls should be operable with gloves where required; locking mechanisms must resist accidental release, and deployment should be repeatable. |
Conduct user trials, repeated deployment cycles, glove-use checks, adjustment backlash measurements, and inspection after contamination exposure. |
5% |
0–10 |
| Documentation and Configuration Control |
Technical drawings, revision history, bills of materials, inspection criteria, packaging requirements, and change-notification procedures should be controlled. |
Review sample approval procedures, engineering-change notices, lot identification, certificates of conformity, and retention periods for quality records. |
5% |
0–10 |


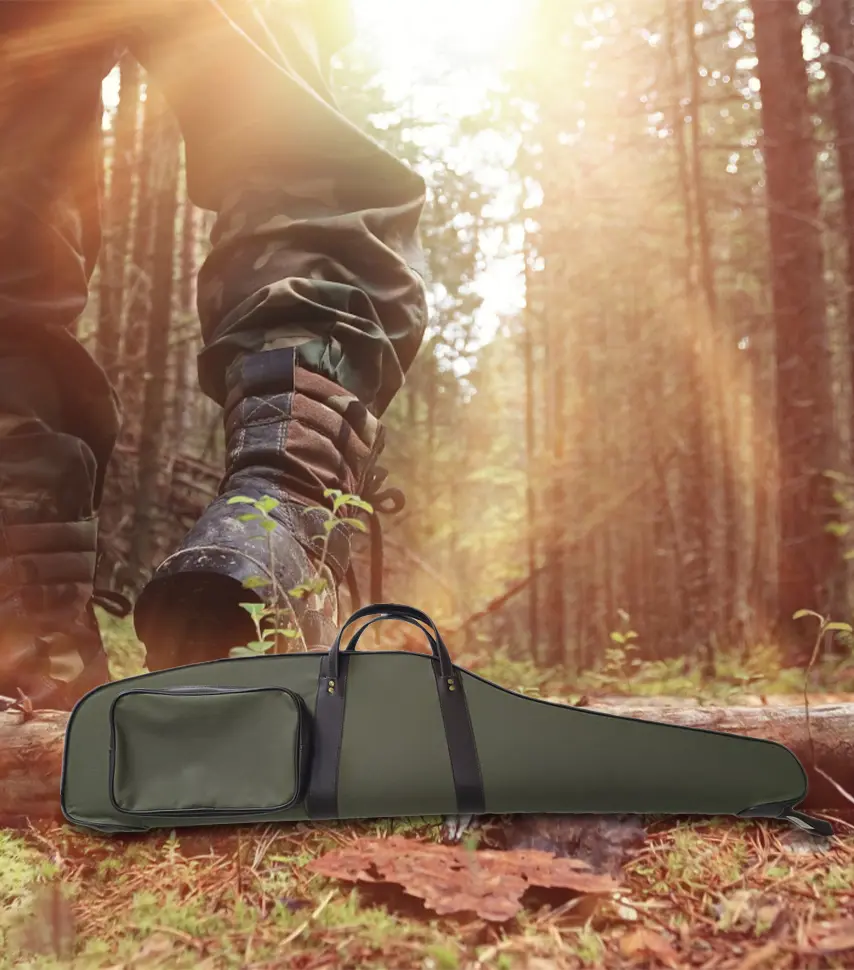 Hunting And Shooting Bag LSH
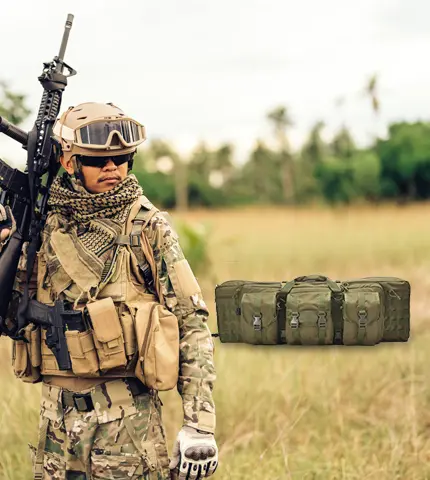 Tactical Military Bag & Vest LST
 Archery Bag LSC
 Fishing Bag LSF
 Others LSB